Judging Exterior Deformation by Depth: Managing Swelling, Wrinkles, Dents, and Impact Marks With Thresholds
Rather than judging based on appearance, judgment becomes stable by defining how many micrometers of deformation constitutes a defect. Using height data from the LJ-X8000 Series, 100% inline judgment of swelling, wrinkles, dents, and impact marks is performed for each cell type.
Inquiries regarding battery exterior deformation and impact mark inspection
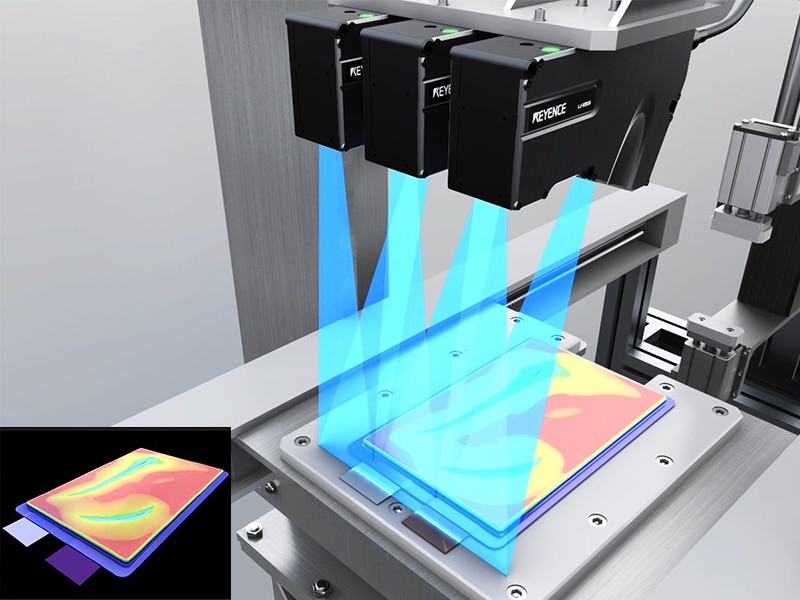
Three Reasons Why Exterior Deformation Inspection Is Unstable
As long as humans judge “whether there is deformation,” the standards will continue to fluctuate.
Deformation Appears Differently Depending on the Cell Type
Since pouch cells use aluminum laminated film, swelling due to internal gas generation and wrinkles during transport and sealing are issues. For prismatic cans, dents on the sides and corners are the main issues, and impact marks caused by transport jigs or handling also appear as similar depressions. Even for the same “exterior deformation,” the measurement method changes depending on whether you look at swelling as a surface or local depressions. If you try to judge under a single condition without separating the cell types, one of them will be missed.
Visual Inspection Standards Depend on the Individual
Visual or image-based appearance inspection results vary depending on lighting conditions and inspector experience. Especially for cell exteriors, there are printed characters, logos, and film gloss, making it difficult to distinguish between deformation and patterns using only contrast. If standards shift from line to line or shift to shift, it is impossible to explain “what was considered acceptable” when a defect occurs later. A system that judges based on physical quantities is required.
Cannot Judge Without a Threshold
Unless you define “from how many micrometers of dent or impact mark a part is considered defective,” you cannot make a judgment even if you can measure it. Thresholds must be determined by calculating backward from assembly interference in subsequent processes or internal effects. By first measuring the distribution of deformation in acceptable lots to understand the current status, and then setting the threshold at a level that differentiates them from defective parts, both over-detection and missed defects can be suppressed.
4 Steps to Determine Thresholds and Perform 100% Inspection
In addition to implementing a measurement system, the process must be designed up to the creation of judgment standards.
- 1 Determine the measurement surface for each cell type – STEP 1. First, determine the measurement surface and evaluation index for each cell type, such as swelling and wrinkles across the entire surface for pouches, and dents and impact marks on the sides and corners for prismatic cans.
- 2 Obtain deformation amount with height data – STEP 2. Obtain height as a 3D image. Since it is not affected by background text or logos, it is less likely to mistake exterior printing for deformation.
- 3 Determine thresholds – STEP 3. Measure the distribution of deformation in acceptable lots to understand the current status, and set the threshold at a level that differentiates them from defective parts. The balance between over-detection and missed defects can be adjusted numerically.
- 4 100% judgment and recording – STEP 4. Reject defective parts based on judgment output, and save NG images and measured values. By keeping these along with the history of threshold changes, the judgment standards can be explained.
Comparison of Exterior Deformation Detection Methods
The key differences lie in whether the deformation amount can be recorded numerically and whether the system is unaffected by printing or gloss.
| Inspection items / Installation requirements | LJ-X8000 Series (3D cross-section profile) |
2D image sensor (2D inspection using grayscale only) |
Visual inspection | Contact gauge |
|---|---|---|---|---|
(1) Pouch cell swelling (surface rise) |
LJ-X8000 Series (3D cross-section profile)
◎ Quantified as surface height distribution
|
2D image sensor (2D inspection using grayscale only)
× Cannot determine height
|
Visual inspection
△ Only large ones
|
Contact gauge
△ Limited to a few points
|
② Pouch cell wrinkles |
LJ-X8000 Series (3D cross-section profile)
◎ Extracted as local height differences
|
2D image sensor (2D inspection using grayscale only)
△ Unstable if there is no contrast
|
Visual inspection
△ Depends on the viewing angle
|
Contact gauge
× Cannot detect
|
③ Dents and impact marks on the side of rectangular cans |
LJ-X8000 Series (3D cross-section profile)
◎ Determine depth numerically
|
2D image sensor (2D inspection using grayscale only)
× Cannot determine depth
|
Visual inspection
△ Judgment depends on the individual
|
Contact gauge
△ Measurement points are limited
|
④ Dents and scratches on corners |
LJ-X8000 Series (3D cross-section profile)
◎ Detect scratches and deformation separately
|
2D image sensor (2D inspection using grayscale only)
○ Scratches are easy to detect
|
Visual inspection
△ Defects are easily overlooked
|
Contact gauge
× Cannot detect
|
⑤ OK/NG threshold setting |
LJ-X8000 Series (3D cross-section profile)
◎ Set/change with numerical values in µm
|
2D image sensor (2D inspection using grayscale only)
△ Uses indirect indicators such as area
|
Visual inspection
× Standards are verbal
|
Contact gauge
△ Only values at a few points
|
Resistance to printing, logos, and gloss |
LJ-X8000 Series (3D cross-section profile)
◎ Not easily affected because it uses height data
|
2D image sensor (2D inspection using grayscale only)
× Patterns are easily misdetected as defects
|
Visual inspection
△ Appearance changes
|
Contact gauge
○ Unaffected
|
Inline 100% inspection |
LJ-X8000 Series (3D cross-section profile)
◎ Supports 100% inspection without positioning
|
2D image sensor (2D inspection using grayscale only)
○ 100% inspection is possible
|
Visual inspection
× 100% inspection is not realistic
|
Contact gauge
× Tact time cannot be met
|
Recording judgment basis |
LJ-X8000 Series (3D cross-section profile)
◎ Saves deformation amount and NG images
|
2D image sensor (2D inspection using grayscale only)
○ Images can be saved
|
Visual inspection
× Difficult to keep records
|
Contact gauge
× Relies on manual recording
|
Reasons to Choose the LJ-X8000 Series for Exterior Deformation Detection
Because the LJ-X8000 Series acquires deformation as a physical quantity of height, thresholds such as “how many µm of depression is considered NG” can be set directly. Dents caused by transport or handling can also be handled using the same depth index. Because height images are not affected by printing or logos on the exterior, or the gloss of the film, patterns are not mistaken for defects. Combined inspection of grayscale and 3D images also allows scratches and deformation to be handled separately.
Products Compatible With Battery Exterior Deformation Detection
This inline profiler quantifies deformation as height, allowing 100% inspection with thresholds in µm units.
Compatible With Deformation Detection of Pouches and Prismatic Cans — LJ-X8000 Series
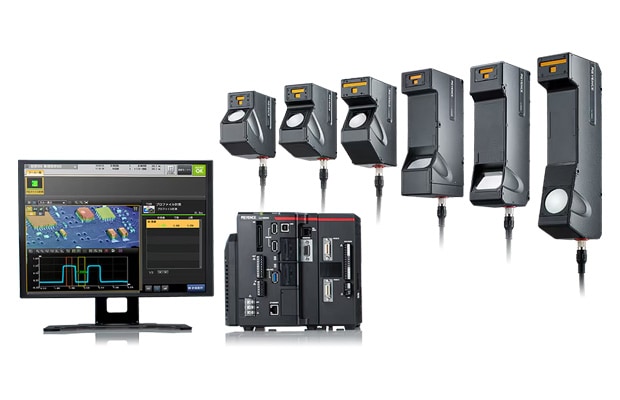
2D/3D Laser Profiler
Ultra-high-definition measurement of 3200 points/profile represents surface shapes in detail, quantifying the amount of deformation as a physical quantity of height. Both overall surface swelling and local depressions such as dents and impact marks can be handled as depth from the same height data. By extracting irregularities from free-form surfaces, only local depressions can be extracted even for targets with slightly curved surfaces.
Because height images generated from height data are not affected by printing or logos on the exterior, or the gloss of the film, patterns are less likely to be mistaken for defects. Because it supports combined inspection that combines grayscale and 3D images, surface scratches and shape deformation can be handled separately. It is less susceptible to changes in distance or height differences, allowing stable imaging even if cell dimensions change due to product changeovers. The 3D position correction function automatically corrects for target misalignment and tilt, eliminating the need for positioning. When combined with the automatic target detection function, inline 100% measurement and inspection can be achieved. It also supports rejecting NG products via judgment output and saving NG images and measured values using the FTP server function, allowing operations that keep judgment criteria and their evidence.
Get Detailed Materials on the LJ-X8000 Series
You can download a free catalog summarizing sensor head specifications, measurement tools, and system configuration.
Inquiries regarding battery exterior deformation and impact mark inspection
Examples of Cell Exterior Inspection Applications
It is used for appearance inspection of various batteries, such as prismatic, pouch, and cylindrical types, to detect dents and scratches.
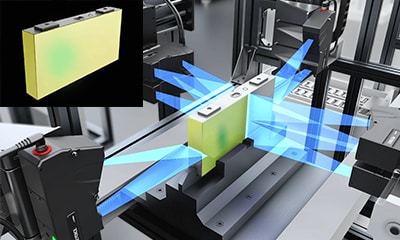
Cell Appearance Inspection (Prismatic)
Performs appearance inspection of individual cells. Dents occurring on corners and scratches on sides are stably inspected using not only grayscale images but also 3D images.
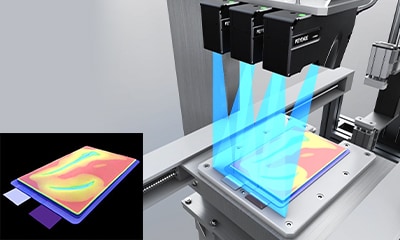
Cell Appearance Inspection (Pouch)
Performs appearance inspection of pouch-type batteries. Because 3D data is image-processed, even gentle dents that are difficult to detect with 2D image processing can be stably inspected.
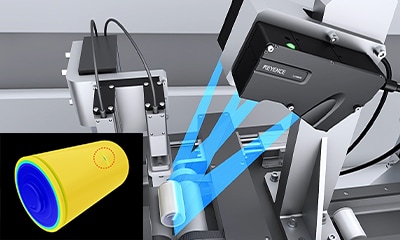
Exterior Can Appearance Inspection (Cylindrical)
Performs appearance inspection of the side of cylindrical batteries. Even for gentle dents that conventional cameras struggle with, the LJ-X8000 Series detects them using height data, enabling stable inspection.
Frequently Asked Questions Regarding Detection of Battery Exterior Swelling, Wrinkles, Dents, and Impact Marks (LJ-X8000 Series)
Q How should the OK/NG threshold be determined?
A
After calculating the required level based on assembly interference in subsequent processes and internal impacts, the distribution of deformation in acceptable lots is measured to understand the current status. Setting a threshold at a level that differentiates them from defective products can suppress both over-detection and missed detections.
Q Does the measurement method change between pouch cells and prismatic cans?
A
Yes, it does. For pouch cells, the focus is on swelling (bulging) across the entire surface and localized wrinkles, while for prismatic cans, it is mainly on dents and impact marks on the sides and corners. For cylindrical cells, gentle dents on the sides are the main focus. It is important to determine the measurement surface and evaluation indicators in advance for each cell type.
Q Are printed text or logos on the exterior falsely detected as defects?
A
No, they are not. Because judgment is based on height data, the system does not react to color information such as printed text, logos, or patterns. Even slight unevenness within the same color can be stably inspected using height information.
Q Can only dents be extracted even if the surface is curved?
A
Yes, they can. By extracting unevenness from free-form surfaces, gentle curves of the surface are treated as the reference, allowing only localized dents on top of them to be evaluated.
Q Can dents and swelling be inspected with the same settings?
A
Although both can be handled using height data, the evaluation indicators are different. Dents are viewed as the depth of localized depressions, while swelling is viewed as the amount of bulging across the entire surface, so the measurement surfaces and thresholds are set separately. You can operate by switching inspection settings while keeping the same sensor configuration.
Q Can the basis for judgment be recorded?
A
Yes, it can. The system supports saving images of NG products and measured value data, which can be stored long-term using the FTP server function. By saving these along with the threshold settings, you can maintain a state where the judgment criteria can be explained.