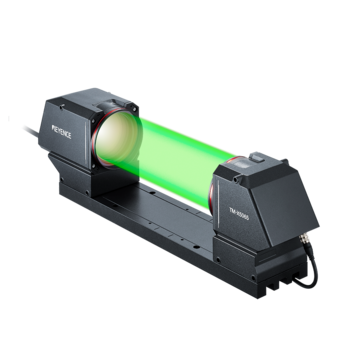
Non-Contact Inline Measurement of Inner Diameters: 100% Inspection of Through-Holes and Rings
Non-contact, inline 100% measurement of inner diameters of through-holes and rings using the transmitted light silhouette method of the TM-X5000 Series telecentric measurement system.
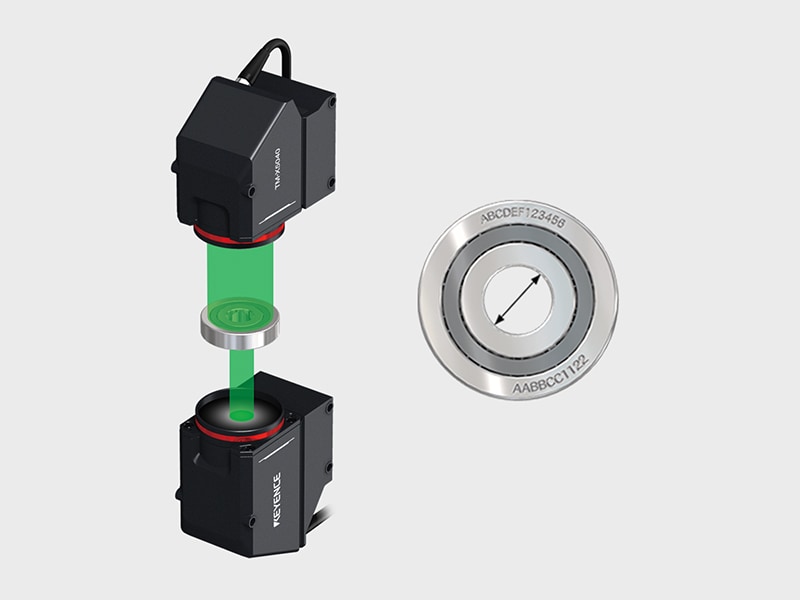
Three Challenges That Arise When Relying on Contact Methods for Inner Diameter Measurement
Contact measurement methods, such as inner diameter gauges and pin gauges, have limitations on-site, leading to defects and losses in 100% inspection and mixed-flow production lines.
Limitations of Contact Methods (Inner Diameter Gauges and Pin Gauges)
Inner diameter gauges, pin gauges, and air micrometers easily deform targets due to measuring force, and values fluctuate depending on how they are applied. Because they focus primarily on go/no-go judgments, it is difficult to record actual dimension trends, and gauge wear calibration costs are also incurred. Errors and oversights caused by measurement methods manifest as press-fitting/mating defects in subsequent processes or a decrease in yield rate, leading to quality variations in final products and difficulty in identifying causes.
Difficult to Implement 100% Inspection and Inline Measurement
Because contact methods measure one point at a time and require stopping, sample inspection inevitably becomes the primary method. On mixed-flow lines, gauges must be changed for each product type, increasing the burden of cycle time, setup, and labor. If variations in inner diameters are missed during sample inspection, defects flow to subsequent processes, resulting in rework and sorting man-hours, and potentially leading to defective final products escaping into the market.
The Optimal Method Changes Depending on the Shape and Size
The suitable measurement method differs between small-diameter through-holes/rings and large-diameter closed inner walls like steel pipes. If the wrong method is chosen, it often results in an inability to measure or a lack of accuracy. It is necessary to select the principle—using either transmitted light silhouette or distance measurement—according to the size and shape of the target. Incorrect selection can lead to re-measurement in subsequent processes or overlooking dimensional defects in final products.
Selecting the Right Method for Each Target in Inner Diameter Measurement
By selecting the measurement method according to the size and shape of the target, inner diameters can be reliably managed without contact.
- 1 Through-holes and rings (small to medium diameters) – Method 1. Non-contact, simultaneous multi-point measurement of inner diameters using the transmitted light silhouette of the TM-X5000 Series. Manage the hole diameters of bearing inner rings and wire drawing dies with 100% inspection.
- 2 Large diameters and steel pipes (closed inner walls) – Method 2. Calculate inner diameters by measuring the distance to the inner wall with a confocal displacement sensor (CL-3000 Series). This approach uses distance measurement for large-diameter targets that cannot transmit light.
- 3 Complex shapes and cross-sections – Method 3. Obtain cross-section profiles with a 3D laser profiler (LJ-X8000 Series) and evaluate inner diameters and circularity based on their shape.
Comparison of Inner Diameter Measurement Methods
There are significant differences in non-contact properties, target sizes, and inline suitability depending on the measurement method.
| Comparison items | TM-X5000 Series (Projection/Transmitted Light / Non-Contact) |
CL-3000 Series (Reflection / Non-Contact) | Contact Method: Inner Diameter Gauges and Pin Gauges | Air micrometer |
|---|---|---|---|---|
Non-Contact / Impact on Workpieces |
TM-X5000 Series (Projection/Transmitted Light / Non-Contact)
○ Non-contact with no deformation
|
CL-3000 Series (Reflection / Non-Contact)
○ Non-contact
|
Contact Method: Inner Diameter Gauges and Pin Gauges
× Deformation/wear due to measuring pressure
|
Air micrometer
△ Non-contact but requires proximity
|
Inner Diameters of Through-Holes and Rings |
TM-X5000 Series (Projection/Transmitted Light / Non-Contact)
○ Simultaneous multi-point measurement using transmitted light silhouette
|
CL-3000 Series (Reflection / Non-Contact)
△ Point-based distance measurement
|
Contact Method: Inner Diameter Gauges and Pin Gauges
△ Contact one point at a time
|
Air micrometer
△ Requires a dedicated nozzle
|
Large-Diameter/Steel Pipe Inner Diameter |
TM-X5000 Series (Projection/Transmitted Light / Non-Contact)
× Difficult due to inner diameter size and length
|
CL-3000 Series (Reflection / Non-Contact)
○ Calculated from inner wall distance
|
Contact Method: Inner Diameter Gauges and Pin Gauges
△ Requires a large gauge
|
Air micrometer
× Difficult to apply
|
Simultaneous Multi-Point/100% Inline |
TM-X5000 Series (Projection/Transmitted Light / Non-Contact)
○ Up to 100 items, no stopping required
|
CL-3000 Series (Reflection / Non-Contact)
○ High-speed sampling
|
Contact Method: Inner Diameter Gauges and Pin Gauges
× Primarily sample inspection
|
Air micrometer
× Primarily sample inspection
|
Role (Area of Expertise) |
TM-X5000 Series (Projection/Transmitted Light / Non-Contact)
◎ Inner Diameters of Through-Holes and Rings
|
CL-3000 Series (Reflection / Non-Contact)
Large diameter/Inner wall distance
|
Contact Method: Inner Diameter Gauges and Pin Gauges
Single-point GO/NO-GO judgment
|
Air micrometer
Diameter variation in close proximity
|
Why Choose the TM-X5000 Series
The TM-X5000 Series uses a transmitted light silhouette to measure the inner diameters of through-holes and rings simultaneously at multiple points without contact, achieving 100% inspection on mixed-product lines through automatic product type identification. For large diameters and inner walls of steel pipes that cannot transmit light, distance measurement with the confocal displacement sensor (CL-3000 Series) complements this, allowing users to choose the appropriate method based on the target size and shape.
TM-X5000 Series Supporting Non-Contact Inner Diameter Measurement
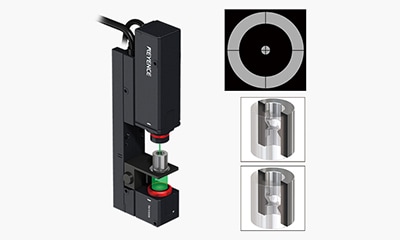
The transmitted light silhouette method with a double telecentric optical system collectively measures the inner diameters of through-holes and rings without contact.
Supporting Non-Contact Inner Diameter Measurement — TM-X5000 Series
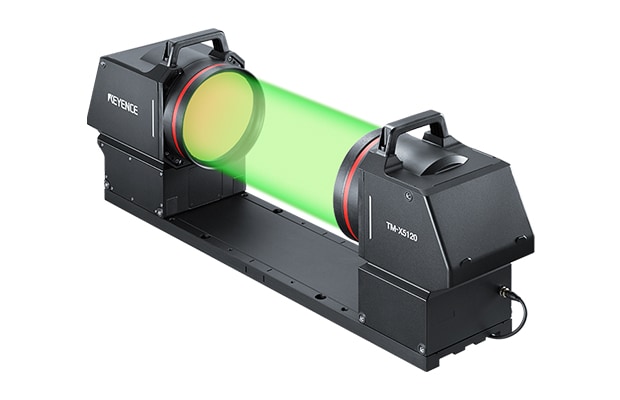
Telecentric Measurement System
The silhouette method (transmitted light) with a double telecentric optical system collectively measures outer diameters, inner diameters, widths, and shapes without contact from the shadows of the target. Up to 100 items can be measured simultaneously in a single shot, and mixed-product lines are supported through automatic product type identification. With high-speed exposure as fast as 25 µs, there is no need to stop even during transfer or rotation. The design requires no calibration, has a wide depth of field, and is highly resistant to misalignment, making inline integration easy. The sensor head can be selected from four models ranging from φ6 to 120 mm. For large diameters and inner walls of steel pipes that cannot transmit light, the confocal displacement sensor CL-3000 Series measures the distance to the inner wall to calculate the inner diameter, allowing users to choose the appropriate method based on the application.
Get Detailed Materials for the TM-X5000 Series
You can download a free catalog containing specifications, system configurations, and application examples.
Application Examples of Non-Contact Inline 100% Inner Diameter Measurement
Inner diameter measurement is utilized in methods suitable for various targets, such as bearings, wire drawing dies, and steel pipes.
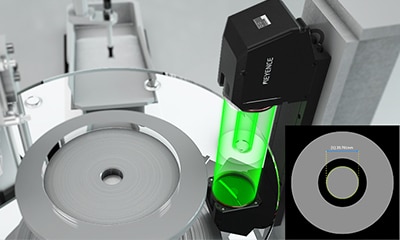
Inner Diameter Measurement of Bearings
The inner diameters of through-holes and rings are measured simultaneously at multiple points without contact using a transmitted light silhouette. 100% of the inner ring inner diameters are managed inline, reducing mating defects.
Inner Diameter Measurement of Wire Drawing Dies
The hole diameters of dies are measured without contact, and diameter expansion due to wear is monitored for 100% of the products. This reduces the labor required to manage die inner diameters, which directly affect wire diameter quality.
Inner Diameter Measurement of Steel Pipes
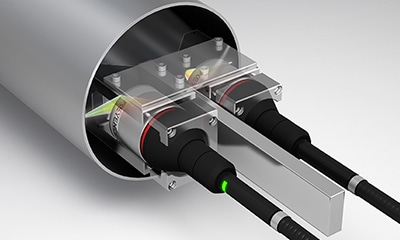
For large diameters and closed inner walls that cannot transmit light, the confocal displacement sensor CL-3000 Series measures the distance to the inner wall to calculate the inner diameter. This allows a non-contact approach even for large targets.
Frequently Asked Questions Regarding Non-Contact Inner Diameter Measurement (TM-X5000 Series)
Q Can inner diameters be measured inline without contact?
A
Yes, they can be measured. The inner diameters of through-holes and rings are measured simultaneously at multiple points without contact using the transmitted light silhouette of the TM-X5000 Series. For large-diameter workpieces and the inner walls of steel pipes, the inner diameter is calculated by measuring the distance to the inner wall using the CL-3000 Series confocal displacement sensor.
Q Can they replace contact-type inner diameter gauges and pin gauges?
A
Yes. The TM-X5000 Series can replace them. Because measurement is non-contact, there is no deformation due to measuring force, gauge wear, or need to switch gauges. In addition to OK/NG judgment, actual dimensions can be recorded for all parts.
Q Can the inner diameters of bearings and wire drawing dies also be measured?
A
Yes, they can be measured. The system supports inner diameter measurement of through-holes and ring shapes, allowing the hole diameters of bearing inner rings and wire drawing dies to be managed for all parts.
Q How do you measure large inner diameters like those of steel pipes?
A
For large-diameter workpieces and steel pipes that cannot transmit light, the inner diameter is calculated by measuring the distance to the inner wall using the CL-3000 Series confocal displacement sensor.
Q Can it be used on multi-product lines?
A
Yes, it can be used. The system recognizes the target shape through automatic product identification and automatically switches the measurement pattern, eliminating the need for product changeover signals or switching gauges.
Q Can measurements be taken without stopping transfer or rotation?
A
Yes, they can be measured. With high-speed exposure as fast as 25 µs, targets can be measured during transfer or rotation without stopping, enabling 100% inline inspection without stopping the line.