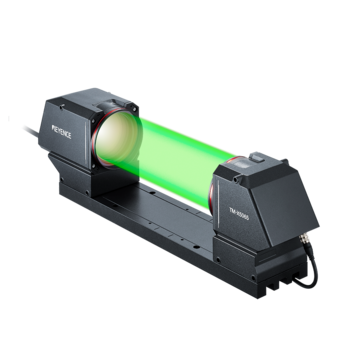
100% Inline Measurement of Screw Dimensions: Inspecting Major Diameter, Outer Diameter, and Pitch Without Stopping
Non-contact, 100% inspection of screw and bolt outer diameters, major diameters, minor diameters, pitch diameters, and pitches using the TM-X5000 Series telecentric measurement system. With a silhouette method using an exposure time as short as 25 μs and a double telecentric optical system, dimensional measurement and OK/NG judgment are performed in-process without stopping the line.
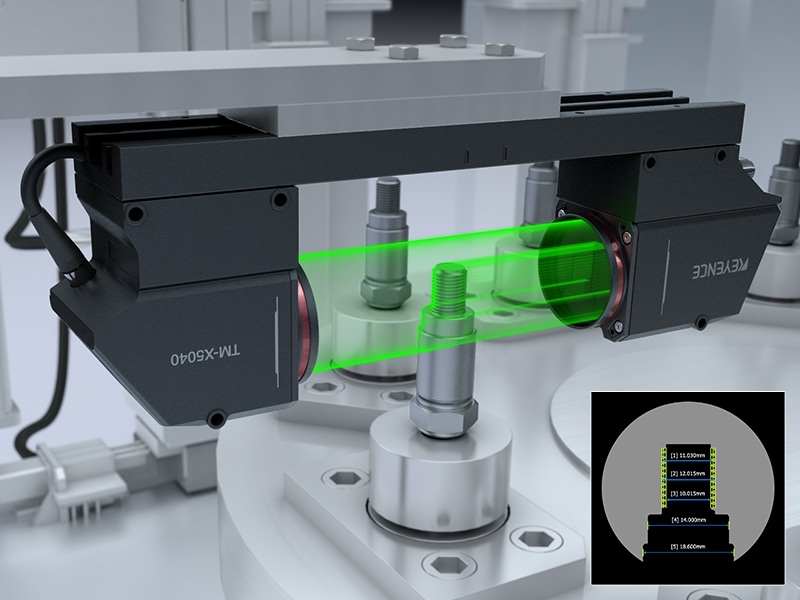
Three Challenges That Arise When 100% In-Process Inspection of Screw Dimensions Is Not Possible
Variations in screw major diameter, pitch diameter, and pitch directly lead to fastening failures. Conventional inspection methods each have their own limitations on the production floor.
Screw Gauges and Sampling Miss Defects
Because go/no-go gauges and micrometers measure parts manually one by one, 100% inspection is not possible. If variations in major diameter, pitch diameter, and pitch slip through sampling, they manifest as fastening failures or galling in subsequent processes or final products. Failure to detect these during the process leads to increased costs due to rework, sorting, and complaints, and also increases the risk of an entire lot escaping.
Conventional Profile Projectors Require Line Stoppages and Manual Labor
Offline profile projectors and image dimension measurements take time because the workpiece must be kept stationary in a measurement room and aligned manually. Because 100% inspection is difficult and cannot keep up with production speeds, in-process quality assurance becomes a bottleneck. Work-in-progress waiting for inspection accumulates, and if defect detection is delayed, it results in massive rework, putting pressure on yield rates and costs.
Contact and Visual Inspections Have Limits in Repeatability and Speed
With contact types, values vary depending on how the contact point is applied, and visual inspection judgments are unstable due to fatigue and individual differences. Multiple items such as screw outer diameter, major diameter, minor diameter, pitch diameter, and pitch cannot be judged against the same standard in a short time, increasing inspection man-hours. If judgment criteria depend on individuals, even good products may be rejected or defects missed, increasing the risk of escapes and the burden of re-inspection.
Screw Manufacturing Process and Key Points of Dimensional Inspection
From thread rolling to recording, screw dimensions and burrs are monitored in-process at each stage to detect variations and defects early.
- 1 Thread Rolling/Cutting – Measurement 1. Measure major diameter, outer diameter, minor diameter, and pitch diameter in-process to detect changes in screw dimensions due to tool wear early.
- 2 Conveyance/Inline Inspection – Measurement 2. Inspect screws during conveyance without stopping them, acquiring the outer diameter, pitch, and thread angle at once using a transmitted silhouette for 100% judgment.
- 3 Foreign Matter/Burr Inspection – Measurement 3. Detect chipped threads, burrs, and chips simultaneously with dimensional measurement. Determine OK/NG on the spot and reject defective products.
- 4 Recording/Tracing – Measurement 4. Record measured values and images for 100% of products for quality control. Use the data to provide feedback for tool changes and process adjustments.
Comparison of Screw Dimension Inspection Methods
Depending on the inspection method, there are significant differences in inline 100% capability, impact on the workpiece, simultaneous multi-item measurement, misalignment tolerance, and foreign matter/burr inspection.
| Comparison Items | TM-X5000 Series (Transmitted Silhouette, Double Telecentric / Inline) |
Offline Image Dimension Measurement / Profile Projector | Screw Gauge (Go/No-Go) | Micrometer (Contact Type) |
|---|---|---|---|---|
Non-Contact / Impact on Workpiece |
TM-X5000 Series (Transmitted Silhouette/Double Telecentric/Inline)
○ Non-contact, no scratches
|
Offline image measurement system/profile projector
○ Non-contact
|
Screw gauge (go/no-go)
× Risk of contact/wear
|
Micrometer (contact type)
× Contact/dependent on how it is applied
|
100% inspection/inline compatible |
TM-X5000 Series (Transmitted Silhouette/Double Telecentric/Inline)
○ 100% inspection without stopping transfer
|
Offline image measurement system/profile projector
× Stopped in measurement room/sample inspection
|
Screw gauge (go/no-go)
× Manual/sample inspection
|
Micrometer (contact type)
× Stopped/sample inspection
|
Simultaneous measurement of multiple items (outer diameter, major diameter, minor diameter, pitch diameter, pitch) |
TM-X5000 Series (Transmitted Silhouette/Double Telecentric/Inline)
○ Batch measurement with dedicated screw tool
|
Offline image measurement system/profile projector
△ Item by item manually
|
Screw gauge (go/no-go)
× Pass/fail only
|
Micrometer (contact type)
× One item at a time
|
Resistance to misalignment and conveyance |
TM-X5000 Series (Transmitted Silhouette/Double Telecentric/Inline)
○ Accuracy remains unchanged with double telecentric optics
|
Offline image measurement system/profile projector
× Alignment required
|
Screw gauge (go/no-go)
△ Dependent on jig
|
Micrometer (contact type)
× Fixing/stopping required
|
Foreign matter/burr inspection |
TM-X5000 Series (Transmitted Silhouette/Double Telecentric/Inline)
○ Detected simultaneously with dimensions
|
Offline image dimension measurement system/profile projector
△ Combined with visual inspection
|
Screw gauge (go/no-go)
× Not possible
|
Micrometer (contact type)
× Not possible
|
Role (area of expertise) |
TM-X5000 Series (Transmitted Silhouette/Double Telecentric/Inline)
◎ Inline 100% inspection of screw dimensions
|
Offline image dimension measurement system/profile projector
High-precision measurement in a metrology room
|
Screw gauge (go/no-go)
Simple on-site Go/No-Go judgment
|
Micrometer (contact type)
Single item of stationary workpiece
|
Reasons to Choose the TM-X5000 Series
The TM-X5000 Series uses a silhouette method with an exposure time as short as 25 µs and a double telecentric optical system to measure the outer diameter, major diameter, minor diameter, pitch diameter, and pitch of screws during conveyance in a non-contact, 100% manner all at once. Accuracy remains unchanged even if there is misalignment, and multiple items are judged inline using dedicated screw tools. Foreign matter and burr inspections can also be performed simultaneously. It replaces the line stops and manual labor required for offline profile projectors, as well as the sampling inspections performed with screw gauges and micrometers, with inline 100% inspection.
TM-X5000 Series Supporting Inline Inspection of Screw Dimensions
A telecentric measurement system using Green-LED transmitted light and a double telecentric optical system. It performs non-contact 100% inspection of screw dimensions during conveyance.
Supporting Inline Inspection of Screw Dimensions — TM-X5000 Series
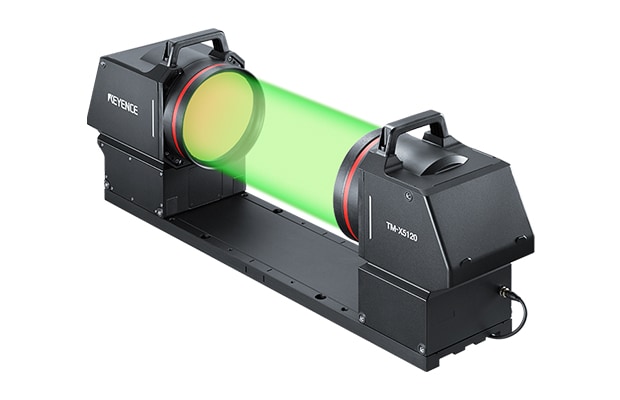
Telecentric Measurement System
With a double telecentric optical system equipped with telecentric lenses on both the transmitter and receiver sides, the silhouette of the screw is imaged from the transmitted light of the Green-LED, and the outer diameter, major diameter, minor diameter, pitch diameter, and pitch are measured without contact. Multiple items, including the thread angle, are acquired at once using dedicated screw tools. Accuracy remains unchanged even if there is workpiece misalignment, and installation is easy with the optical axis alignment function, allowing operation without adjustment or calibration. Workpieces during conveyance can be measured without stopping, and inspections for foreign matter, burrs, and chipping are performed simultaneously. Sensor heads can be selected according to the application, from φ6 mm models to φ120 mm models, replacing sampling inspections and line stops required for screw gauges and offline profile projectors with in-process 100% inspection.
Get Detailed Materials on the TM-X5000 Series
You can download a free catalog summarizing specifications, system configurations, and application examples.
Application Examples of Inline Inspection of Screw Dimensions
These are application examples of 100% inspection of dimensions for various workpieces, such as screws, bolts, and stepped shafts, within the process.
Inline Measurement of Solenoid Valve Screw Dimensions
Non-contact 100% measurement of pitch diameter, outer diameter, minor diameter, pitch, and thread angle using a dedicated screw tool. This inlines conventional screw gauge inspections within the process.
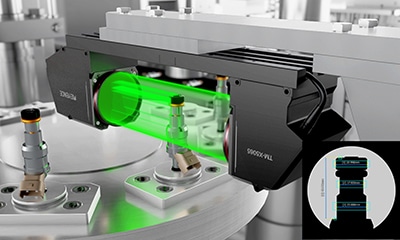
Multi-Point Outer Diameter Measurement of Screw Parts During Index Feeding
Measurement of multiple points on rotating or index-fed workpieces while correcting their positions. This achieves 100% inspection without the need for a dedicated inspection station.
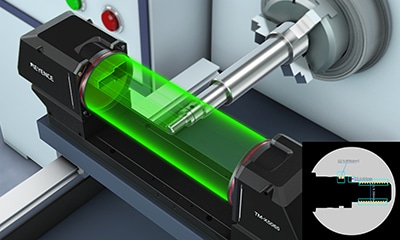
Outer Diameter Measurement of Shaft Screw Threads and Foreign Object Inspection
Measurements are taken while rotating the workpiece, simultaneously measuring the shaft outer diameter of the screw portion and inspecting for burrs and foreign objects.
Frequently Asked Questions About Inline Inspection of Screw Dimensions (TM-X5000 Series)
Q Can dimensions be inspected without stopping the screws during conveyance?
A
Yes, you can. The TM-X5000 Series images screws during conveyance with an exposure time as short as 25 µs, performing non-contact 100% measurement of outer diameter, major diameter, and pitch.
Q Can this replace screw gauge inspections?
A
Yes, it can. By measuring the pitch diameter, outer diameter, minor diameter, pitch, and thread angle all at once with a dedicated screw tool, sampling and manual judgment using go/no-go gauges can be converted into inline 100% inspection.
Q Which screw dimensions can be measured?
A
Outer diameter, major diameter, minor diameter, pitch diameter, and pitch can be measured, and the thread angle is also obtained using a dedicated screw tool. Multiple items are judged at once using a transmitted silhouette.
Q Can measurements be taken accurately even if the workpiece position is misaligned?
A
Yes, they can. The double telecentric optical system provides a deep depth of field, so even if there is workpiece misalignment, the edges do not blur and the accuracy remains unchanged.
Q What is the difference from offline profile projectors or image measurement?
A
While profile projectors are designed for stationary, manual measurement in a measurement room, the TM-X5000 Series can perform 100% inspection on the production line without stopping the screws during conveyance.
Q Can burrs and chipping on screw threads also be detected?
A
Yes, they can. Portions with large differences from the profile are recognized as burrs, chips, or foreign objects, and OK/NG judgment is performed within the process at the same time as dimensional measurement.
Q Please feel free to contact us about challenges with inline inspection and 100% inspection of screw dimensions.
A
Measurement methods, installation configurations, and specifications can be confirmed in the catalog or via the contact form.